
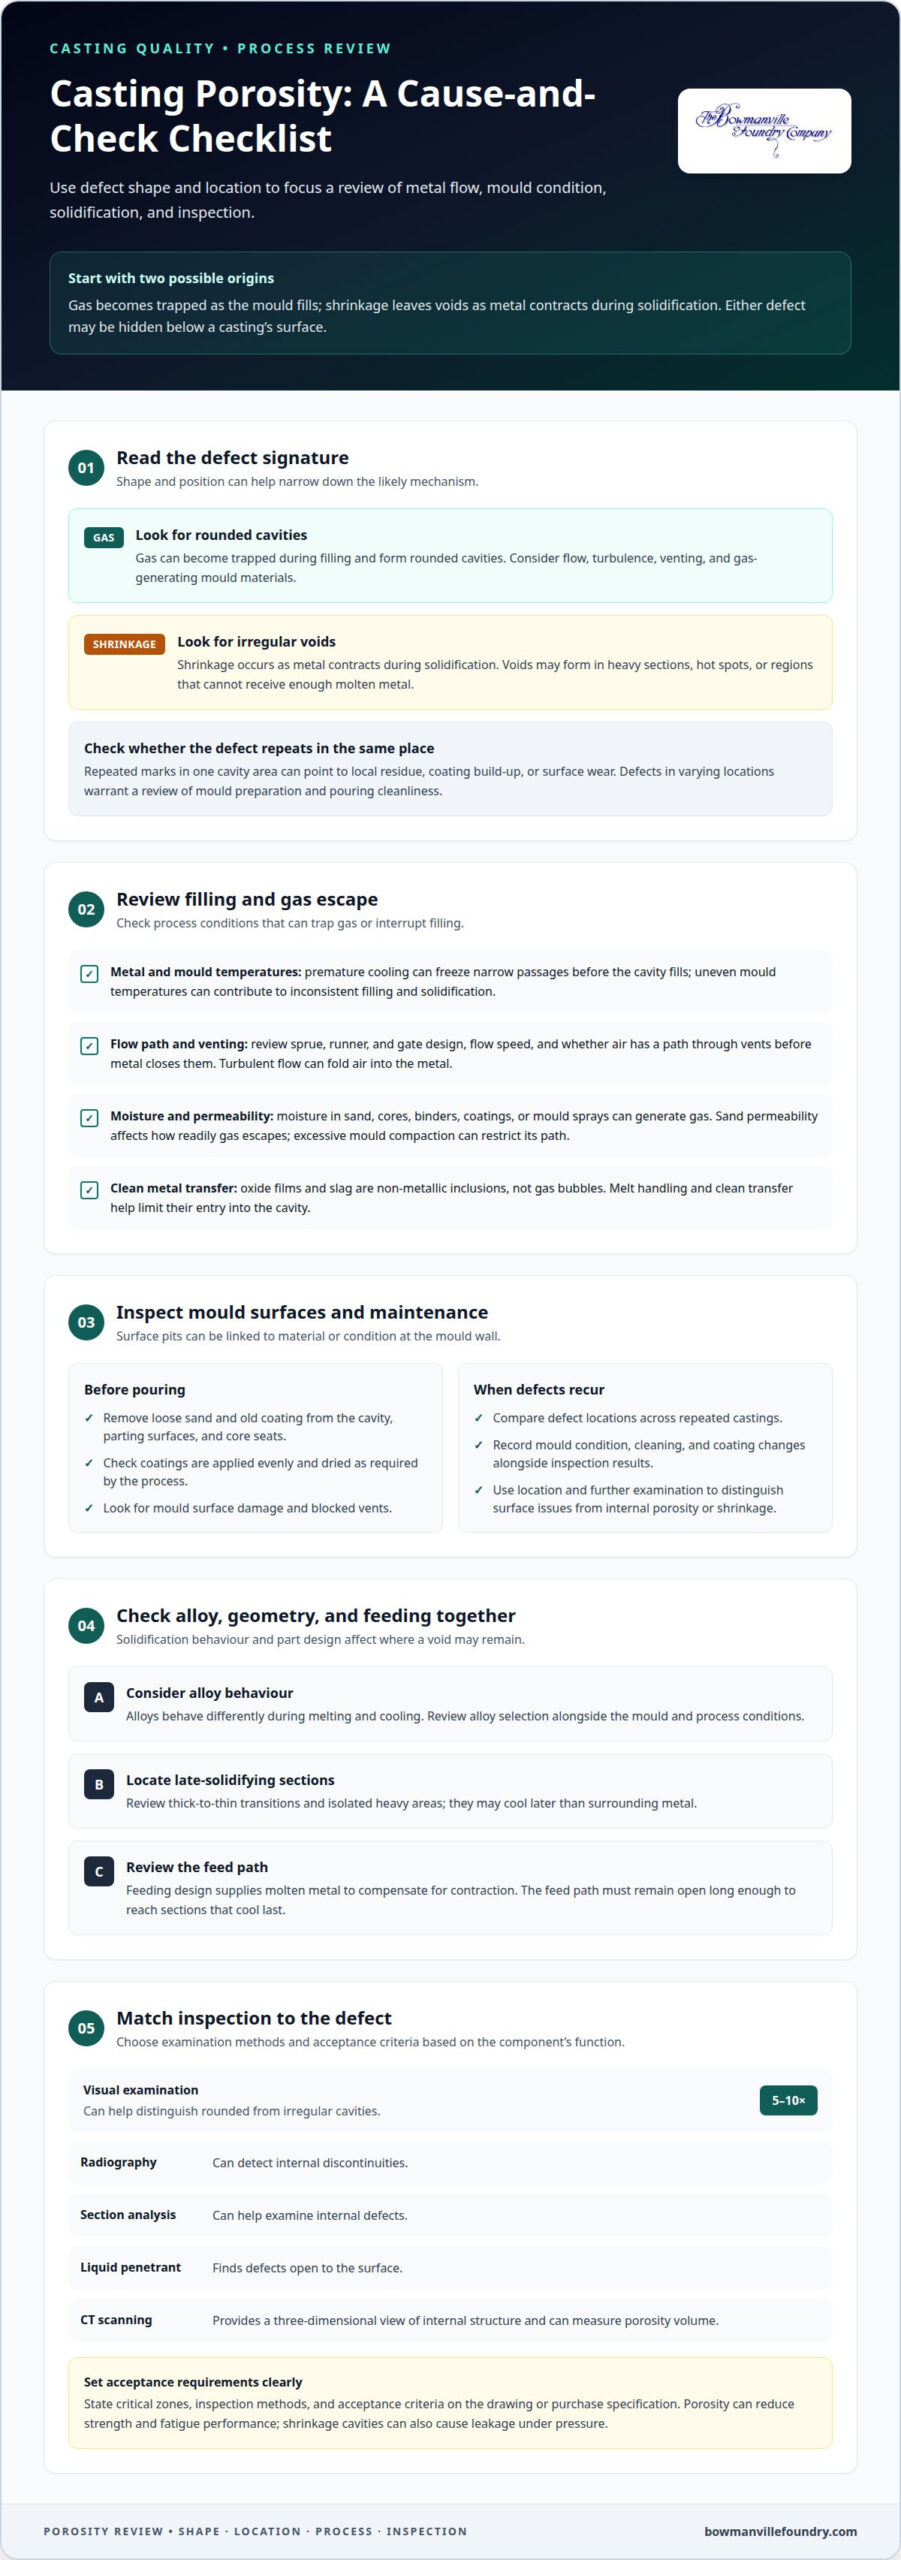
The main causes of casting porosity are gas trapped in the metal or mould and shrinkage as metal cools and solidifies. Gas can form rounded cavities, while shrinkage often leaves irregular voids in areas that solidify last or lack an adequate supply of molten metal. Both defects can occur beneath the surface, affecting a casting’s integrity without appearing in an initial visual inspection.
This article explains how gas and shrinkage porosity develop, how process conditions and mould maintenance contribute, and why alloy and part design should be considered together. Identifying the likely cause helps engineers and casting buyers assess defects and focus on the relevant production factors.
Key Takeaways
- Distinguish rounded gas cavities from irregular shrinkage voids to narrow down the likely defect mechanism.
- Assess metal and mould temperatures alongside flow and venting, since process conditions can trap gas or leave the mould incompletely filled.
- Consider surface contamination and mould condition when porosity appears at the casting exterior.
- Review alloy behaviour and part geometry together to identify where solidification and feeding may need closer attention.
What Causes Gas Porosity and Shrinkage Porosity?
The causes of casting porosity generally fall into two groups: gas trapped as the mould fills, and voids left as metal contracts. Defects may be visible on the surface or hidden inside the casting, so both their location and shape matter.
Shrinkage during solidification
Shrinkage occurs as metal contracts during solidification. If liquid metal cannot reach a region that is still cooling, a cavity may remain, often in a heavy section or near a hot spot. The causes of casting porosity matter to buyers because an internal void can affect a critical machined face or sealing area, even when the exterior looks sound. The European Union’s StaCast classification distinguishes gas porosity from solidification shrinkage by their metallurgical origin.
Feeding design and shrinkage prevention
Feeding design supplies additional molten metal to compensate for contraction as the casting solidifies. The feed path must remain open long enough to supply sections that cool last. Review thick-to-thin transitions and isolated heavy areas in the part geometry, since they may solidify later than surrounding metal. The causes of casting porosity can inform design review, particularly when voids repeatedly appear in the same region.
Rounded cavities can indicate gas porosity, while irregular cavities can indicate shrinkage. Visual examination under 5-10x magnification can help distinguish them, but internal defects may need radiography or section analysis.
For Canadian projects, state acceptance requirements on the drawing or purchase specification. Identify critical zones, inspection methods, and acceptance criteria based on the component’s function.
Radiography can detect internal discontinuities, while liquid penetrant testing finds defects open to the surface. CT scanning provides a three-dimensional view of internal structure and can measure porosity volume.
Porosity can reduce strength and fatigue performance by creating stress concentrations. Shrinkage cavities can also cause leakage under pressure, even when machining leaves a surface that looks sound.
Repair depends on defect location and the agreed acceptance criteria. Impregnation may seal leakage paths in suitable castings. Reject a part when defects exceed specified limits or compromise its required function.
Effects of molten-metal and mould temperatures on gas entrapment
Temperature affects how molten metal fills a mould and how long gases have to escape. If metal cools too quickly during filling, narrow passages may freeze before the cavity is full. Excessive turbulence can fold air into the metal, trapping bubbles as the casting solidifies. The appropriate method depends on alloy behaviour, mould geometry, and the required flow path.
Mould temperature also affects heat transfer and gas release. A cold region can cause premature cooling, while uneven temperatures may lead to inconsistent filling and solidification. Review metal and mould temperatures alongside sprue, runner, and gate design. These factors influence flow speed and whether air has a clear path through vents before metal closes them.
In sand castings, moisture in the mould can turn to vapour on contact with molten metal. Sand permeability determines how readily the gas escapes; excessive mould compaction or unsuitable sand characteristics can restrict its path. Moisture in cores, binders, coatings, or mould sprays can also generate gas at the metal interface. Dry, controlled mould materials and clear vents help manage this mechanism.
Core and binder reactions can produce additional gas. For example, a coating that releases gas during pouring may create local bubbles where metal contacts the core. Injection speed and pouring turbulence matter too: forceful flow can entrain air, while a well-designed gating system guides metal smoothly. Vacuum methods aim to reduce the amount of gas trapped during filling.
Non-metallic inclusions, such as oxide films or slag carried into the cavity, differ from gas bubbles but can disrupt casting integrity. Melt handling and clean transfer help limit their entry. For iron casting material guidance, review iron casting information alongside the process factors affecting gas entrapment.
Surface contamination and mould maintenance
Contaminants on a mould surface can produce surface porosity during casting. Examples include loose sand, coating residue, moisture, oil, or debris. These materials may react with hot metal or interfere with contact at the mould wall, leaving visible pits or cavities. Because the defect begins at the surface, its position can help distinguish it from shrinkage porosity or internal porosity deeper inside the casting.
Mould maintenance helps control surface conditions. Before pouring, remove loose sand and old coating from the cavity, parting surfaces, and core seats. Check that coatings are applied evenly and dried as required by the process. A damaged mould surface or blocked vent can affect metal contact and gas escape. For example, recurring pits beside one core seat may indicate local residue or surface damage rather than a general melt issue.
Relate process observations to defect locations. If marks appear in the same cavity area across repeated castings, inspect for adhered sand, coating build-up, or wear. If defects appear in varying locations, review handling and cleanliness during mould preparation and pouring. This comparison helps direct testing: visual inspection records where defects appear, while further examination can establish whether they extend inside the casting.
Good maintenance also supports reliable evaluation of casting strength. Record mould condition, cleaning, and coating changes alongside inspection results so you can compare a process adjustment with the next production run. Do not assume every cavity is a mould defect: internal porosity and shrinkage porosity have different origins. A location-based review helps distinguish surface contamination from defects formed during filling or solidification and directs corrective action to the relevant stage.
Alloy selection and porosity risk
Alloy selection affects how molten metal flows, cools, and solidifies in a mould. Gray Iron, Ductile Iron, and Malleable Iron have distinct material characteristics, so a grade suited to one component may not suit another. Porosity risk depends on the alloy, casting geometry, and production conditions together. Define the component’s loading, service environment, and critical surfaces before choosing a material.
Consider the part’s thick sections, thin walls, and transitions. A heavy boss connected to a thin wall can cool unevenly, while a long flow path can make complete filling more difficult. These features can increase the chance of defects if gating and feeding are not matched to the design. Reviewing the casting drawing alongside the intended alloy helps identify where solidification and metal flow need attention.
Machining plans also affect the impact of porosity on the finished component. A machined face may expose pores hidden on the as-cast surface, particularly when the machining allowance removes material from a critical zone. Mark sealing faces, pressure-related areas, and structural features on the drawing. Then align inspection with those locations instead of relying only on a general visual review.
When selecting an alloy, compare the required properties with the part geometry and manufacturing route. Material choice alone cannot prevent gas or shrinkage defects; melt handling, mould conditions, gating, and feeding also matter. If inspection finds recurring porosity, compare defect locations across castings and relate them to section thickness, flow paths, and machining surfaces. This evidence helps focus process review on the likely cause.
Use the Free Casting Buyer’s Guide to support material and casting discussions, or contact Bowmanville Foundry about Gray Iron, Ductile Iron or Malleable Iron Castings.
Bowmanville Foundry: Malleable Iron Castings
Bowmanville Foundry produces Malleable Iron Castings for buyers assessing iron materials and casting requirements. Malleable Iron is used for small castings that need good tensile strength and ductility. Discuss the component’s geometry, service conditions, and critical machined areas when considering material selection and porosity acceptance.
For parts better suited to another iron grade, Bowmanville Foundry also produces Gray Iron Castings and Ductile Iron Castings. Post-Processing Services are available for customers who need finishing work alongside their castings. Sharing the part drawing and inspection requirements can help frame a productive technical discussion about the application.
Contact Bowmanville Foundry or visit bowmanvillefoundry.com to discuss your casting requirements.
Make porosity requirements part of the next design discussion
Understanding the causes of casting porosity is most useful when findings inform decisions before production moves forward. Turn inspection observations into clear drawing notes and acceptance criteria. Mark critical areas, such as machined faces or sealing surfaces, so requirements reflect how the finished component will function.
For a new or revised part, bring the drawing, service conditions, machining requirements, and inspection expectations into the same technical discussion. This gives design and procurement teams a shared basis for reviewing material suitability and production needs. It also keeps casting decisions aligned with the component’s intended use.
Bowmanville Foundry can discuss iron casting requirements for your application. Contact Bowmanville Foundry to begin a practical conversation about your project. A clear technical brief is a constructive next step toward a well-defined casting specification.
Frequently Asked Questions
How Can Mold Design and Process Control Reduce Porosity Risk?
Reduce risk by turning the part drawing into a documented review and inspection plan. Mark critical faces, machining allowances, and sealing areas, then identify where inspection results need to be recorded. During production, compare defect locations across castings and against cavity positions. This helps show whether an issue recurs in one part feature or varies between runs, giving process reviews a clear, evidence-based starting point.
What are the common types of porosity found in cast metals?
Common categories include gas porosity, shrinkage porosity, surface porosity, and internal porosity. For a useful inspection record, describe more than the category: note the defect’s location, shape, distribution, and whether machining exposed it. For example, document a single cavity on a machined face differently from scattered indications across several areas. This detail supports consistent comparison with the drawing’s acceptance criteria.
What is Blowhole (Gas Porosity)?
A blowhole is a relatively large, rounded cavity associated with gas in a casting. Record its position and extent, especially if it lies on a machined, pressure-related, or sealing surface. The name alone does not establish whether the casting is acceptable. That decision depends on the specified inspection requirements and the defect’s effect on the part’s intended function.
What causes gas porosity in metal casting?
Gas porosity occurs when gas remains in the casting instead of escaping before the metal solidifies. To investigate a defect, compare its position with the mould cavity, cores, and melt-handling records. A consistent location across parts can point to a localized process condition, while varying locations may call for a broader review of production records. This evidence helps narrow the investigation without assuming a single cause.
How do turbulence and poor gating cause air entrapment in castings?
Turbulence and unsuitable gating can trap air in a casting, but a defect map is more useful than a general process assumption. Record where indications occur relative to gates, runners, and cavity features, then compare that pattern with pouring observations. If the same region is affected repeatedly, review the local flow arrangement. If locations vary, examine run-to-run production records for differences.
How do shrinkage and inadequate feeding cause casting porosity?
Shrinkage porosity occurs when contraction during solidification is not offset by an adequate supply of molten metal. To assess a suspected defect, compare its position with section thickness and the casting’s feeding layout. A recurring cavity in a heavy area can guide a design or process review. Acceptance still depends on the component’s specified limits and whether the affected region is functionally critical.
